Non-Halogen Flame Retardancy Solutions
As a next-generation halogen-free flame retardant, Mg(OH)₂ decomposes at 340-490°C releasing 31% by weight water vapor, absorbing 1450 J/g heat while forming an MgO protective layer. Compared to traditional halogen/antimony flame retardants, Mg(OH)₂ is non-toxic and non-corrosive, reducing smoke density by 70-80%, fully complying with EU RoHS and REACH regulations. At 55-65% loading in polyolefins, EVA, and unsaturated polyester, it achieves UL94 V-0 rating, meeting stringent fire safety requirements in construction, transportation, and electronics.
Achieves highest flame retardancy rating at 55-65% loading
Smoke density <100, 70-80% reduction vs halogenated FR
No halogens or antimony, compliant with EU regulations
Abundant raw materials, 30-40% lower cost than brominated FR
From lab to production line, our solutions have been validated in leading global enterprises
In wire/cable jackets and building pipes, modified Mg(OH)₂ achieves balance between flame retardancy and mechanical properties.
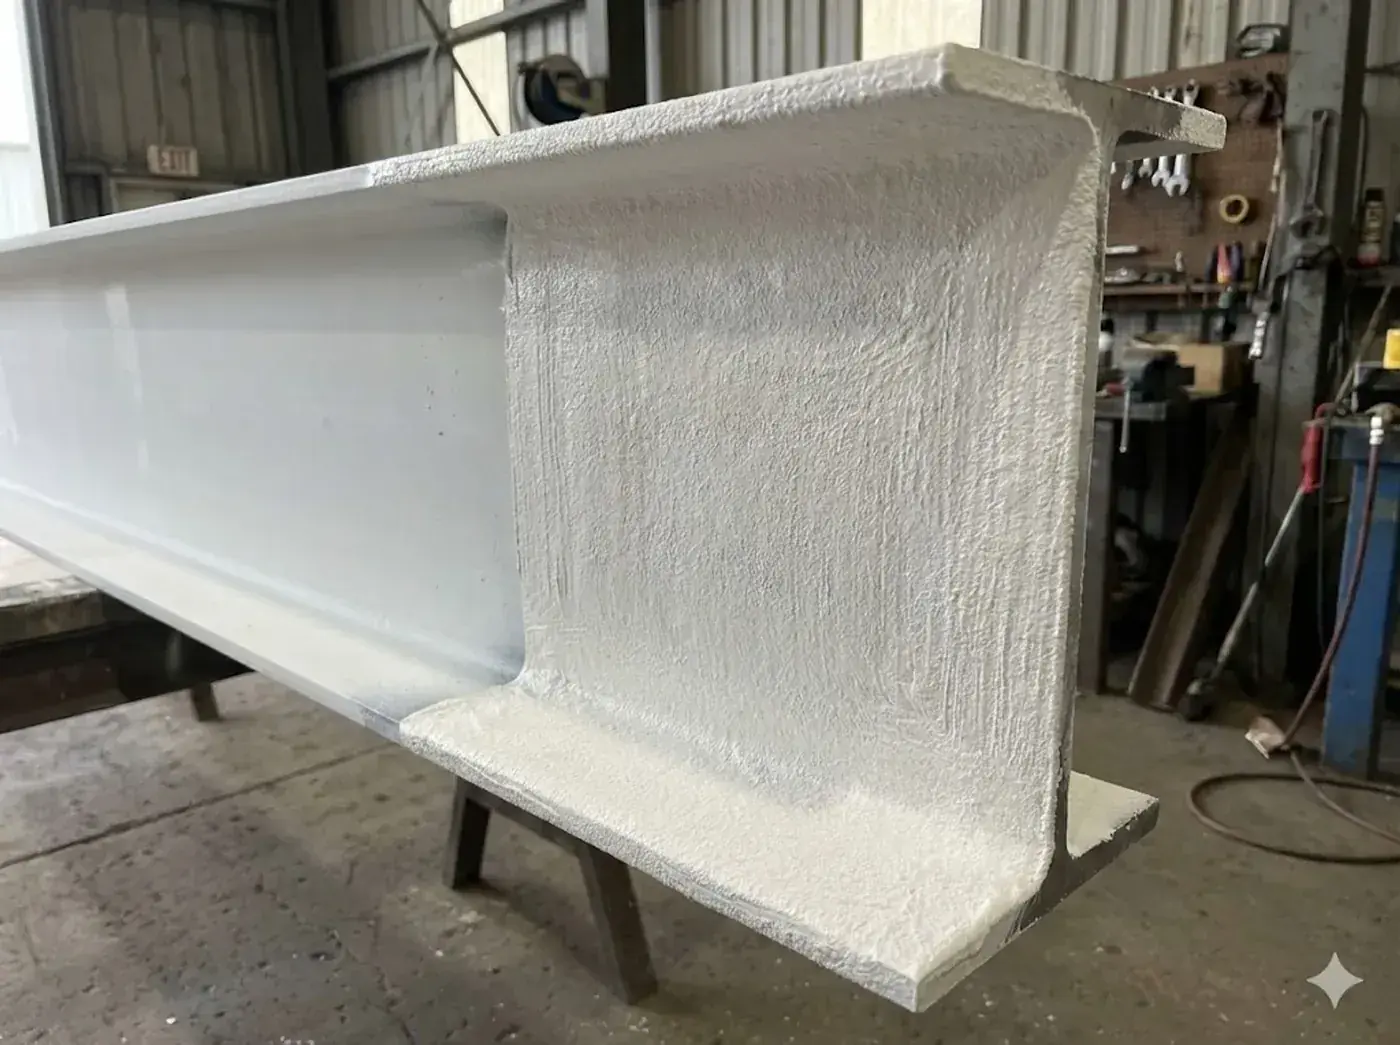
In steel structure fire-resistant coatings, Mg(OH)₂ synergizes with APP/MEL systems, providing 2-hour fire resistance.
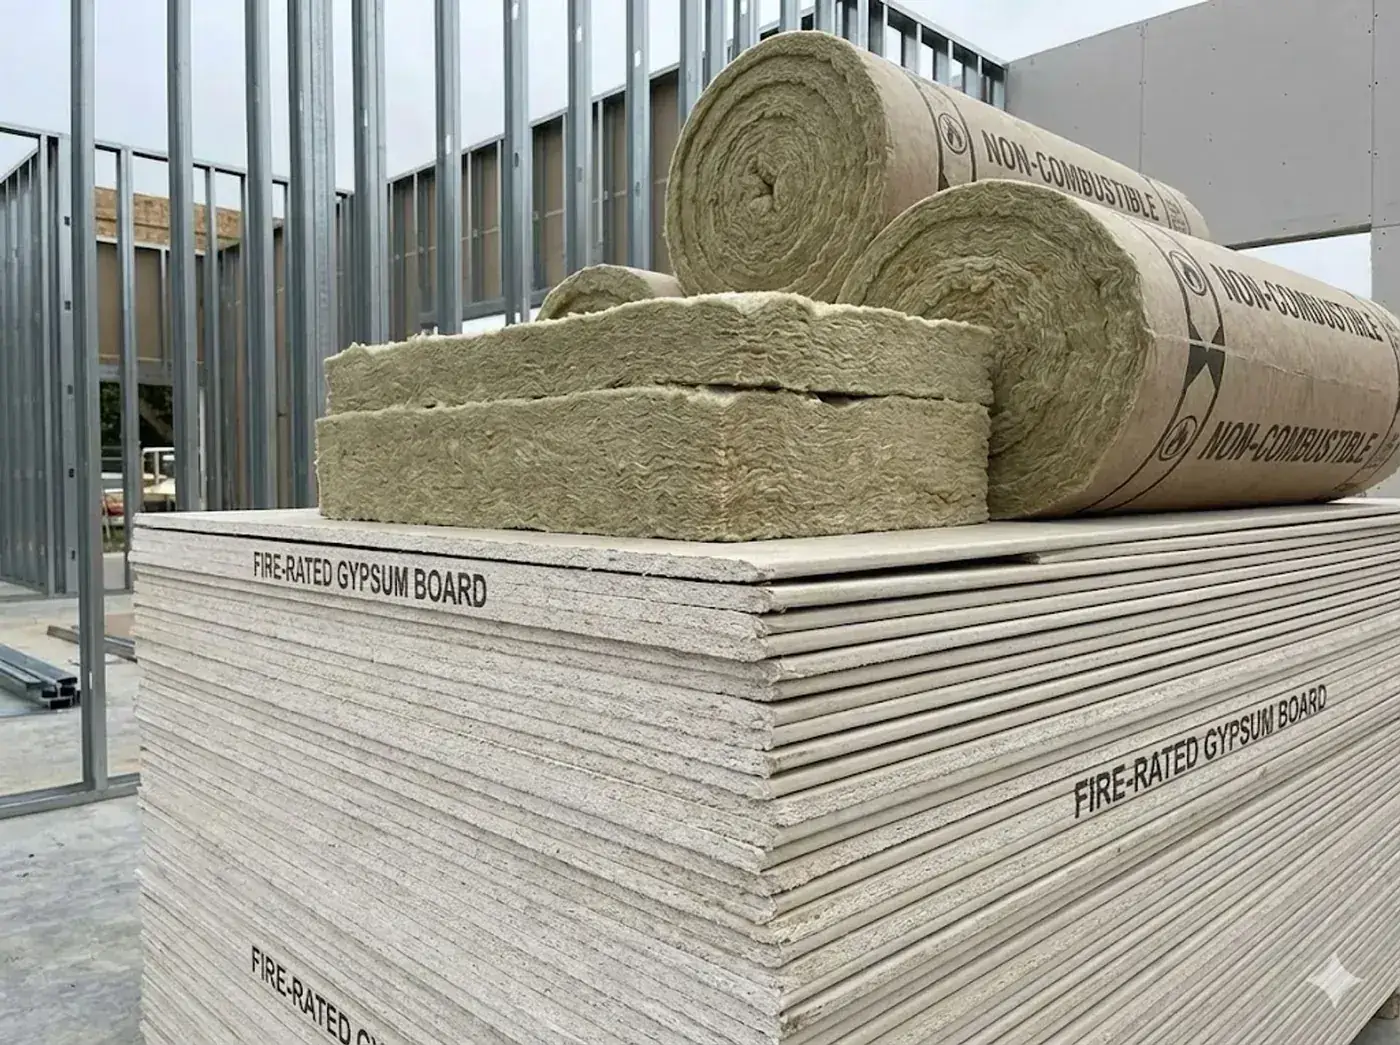
Adding Mg(OH)₂ to decorative panels, insulation materials, and flooring achieves B1-A2 grade fire performance.
High-speed rail, subway, aircraft interiors must meet stringent EN 45545-2 HL2/HL3 standards, Mg(OH)₂ is the preferred choice.
Flame Retardants
Silane/stearate-modified Mg(OH)₂ achieving 60 wt% loading in PE with <30% impact loss, MFI >0.5 g/10min, and UL94 V-0 at 1.6mm thickness.
Why Recommended
Silane/stearic acid dual-modified, 60% loading maintains >70% impact strength, UL94 V-0@ 1.6mm
Flame Retardants
Non-halogenated magnesium hydroxide flame retardant (MDH) releasing 31% H₂O by weight at 340-490°C, achieving UL94 V-0 at 55-65 wt% loading in EVA/PE cables with smoke density <100.
Why Recommended
99%+ purity, D50 1.5-2.0μm, 97% whiteness, suitable for premium FR products
Coatings
Coatings-grade Mg(OH)₂ (1250 mesh, pH 9-10) enabling 2-hour fire resistance, 30% char expansion, and 10-year outdoor durability in intumescent systems.
Why Recommended
1250 mesh ultrafine powder, 30x expansion ratio, 2-hour fire rating, 10-year weatherability
Cable Industry
LSZH-certified Mg(OH)₂ (D50 1.2μm, soluble Na <0.01%) delivering smoke density <50, halogen acid <0.5%, and 72h water treeing resistance at 12 kV.
Why Recommended
D50 1.2μm, smoke density <50, meets EN 45545-2 HL2 requirements
| Performance | Mg(OH)₂ | Al(OH)₃ | Brominated FR | Phosphorus FR |
|---|---|---|---|---|
| Flame Retardancy | UL94 V-0 | UL94 V-0 | UL94 V-0 | UL94 V-1 |
| Loading (wt%) | 55-65 | 60-70 | 10-20 | 15-25 |
| Smoke Density | <100 | 100-150 | >400 | 150-200 |
| Toxicity | None | None | High (HBr/HCl) | Medium (POx) |
| Decomposition Temp (°C) | 340-490 | 220-240 | 200-350 | 250-350 |
| Mechanical Impact | Medium | Large | Small | Medium |
| Regulatory Compliance | RoHS/REACH | RoHS/REACH | Restricted | Partially Restricted |
PP/PE based interior panels needed EN 45545-2 HL2 rating, original halogenated FR solution was banned.
Adopted 'Modified Mg(OH)₂ 60% + red phosphorus synergist 5%' halogen-free formula.
EPS insulation boards needed upgrade from B2 (flammable) to B1 (flame-retardant), traditional HBCD flame retardant was banned.
Switched to 'Mg(OH)₂ 25% + expandable graphite 10%' composite system.
EU RoHS and REACH strictly restrict halogenated flame retardants. Construction, electronics, automotive industries are shifting to halogen-free solutions like Mg(OH)₂.
Nano-grade Mg(OH)₂ with D50<100nm achieves V-0 at 40-50% loading, maintaining >80% mechanical properties.
Mg(OH)₂ + intumescent FR (IFR) + nano-clay ternary synergy achieves integrated flame retardancy, smoke suppression, and low toxicity.
Xingtai Zhongyao's technical team has extensive industry experience and can provide professional formula suggestions and technical support based on your specific application needs.
